| Supplier Definition |
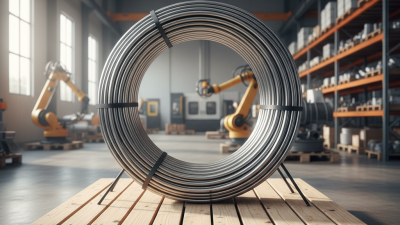
Confirm that the supplier can manufacture or source, inspect, and deliver stainless steel tubing supplied in continuous coils. |
A qualified supplier should provide product specifications, material traceability, dimensional inspection, surface-finish information, and packing details for coiled tubing. |
A coil-tube supplier is more than a trading contact; technical control and traceability are essential for consistent performance. |
| Material Grades |
Check whether the supplier offers grades suitable for the temperature, corrosion, pressure, and forming requirements of the application. |
304 / 304L
316 / 316L
321
2205
304 generally contains about 18–20% chromium and 8–10.5% nickel. 316L typically includes 2–3% molybdenum for improved resistance to chlorides.
|
The wrong alloy can lead to premature corrosion, cracking, or loss of mechanical strength. |
| Applicable Standards |
Request the exact manufacturing and inspection standard stated on the quotation and test certificate. |
Common references include ASTM A213 for seamless boiler, superheater, and heat-exchanger tubes; ASTM A269 for general-service austenitic tubing; ASTM A789 for ferritic and austenitic alloy tubing; and EN 10216-5 for seamless stainless steel tubes.
|
Standards define requirements for chemistry, dimensions, mechanical properties, testing, and acceptance criteria. |
| Outside Diameter |
Confirm the required outside diameter, tolerance, ovality, and measuring method. |
Small-diameter coiled tubing is commonly produced in approximately 3–25.4 mm outside diameters, although available sizes depend on the manufacturing route and grade. |
Diameter affects flow capacity, heat-transfer area, fitting compatibility, and pressure calculations. |
| Wall Thickness |
Verify nominal wall thickness, minimum wall thickness, tolerance, and the effect of bending or coiling on the finished wall. |
Common coiled-tube wall thicknesses are approximately 0.3–3.0 mm. The supplier should state the applicable tolerance rather than quoting only a nominal value. |
Wall thickness directly influences pressure resistance, flexibility, weight, and service life. |
| Coil Length |
Check the requested length per coil, permitted welds, maximum coil weight, and transport limitations. |
Coil lengths are project-dependent. A quotation should clearly identify whether the length is nominal, guaranteed, or subject to a specified tolerance. |
Longer continuous lengths can reduce field joints, installation time, leakage points, and material waste. |
| Manufacturing Method |
Determine whether the tube is seamless, welded, or welded and redrawn, and ask how forming and heat treatment are controlled. |
The manufacturing method should match the applicable standard and service conditions. Welded tubing should include controls for weld integrity, alignment, and post-weld processing where required. |
Manufacturing route affects surface quality, dimensional consistency, pressure capability, and suitability for bending. |
| Surface Finish |
Specify internal and external finish, pickling or bright-annealed condition, roughness requirement, and cleanliness level. |
Common descriptions include annealed and pickled, bright annealed, and mechanically polished. If roughness is critical, request a measurable Ra value and inspection method. |
Surface condition affects corrosion resistance, cleanability, friction, fluid contamination, and appearance. |
| Mechanical Properties |
Review tensile strength, yield strength, elongation, hardness, and the condition in which the values are guaranteed. |
For austenitic stainless steel tubing, the required values depend on the grade, product standard, and heat-treatment condition. The values should appear on the material test certificate. |
Mechanical properties indicate whether the tube can withstand forming, vibration, pressure, and operating loads. |
| Pressure and Leak Testing |
Ask which tests are included and whether test pressure, duration, acceptance criteria, and records are documented. |
Depending on the standard and application, inspections may include hydrostatic testing, pneumatic testing, eddy-current testing, ultrasonic testing, and visual examination. |
Testing helps identify leaks, weld defects, laminations, and other discontinuities before shipment. |
| Chemical Traceability |
Confirm heat-number identification from raw material through production, testing, packing, and shipment. |
A complete EN 10204 3.1 material certificate normally includes heat number, chemical composition, mechanical results, product standard, and authorized inspection confirmation. |
Traceability supports quality investigations, regulatory documentation, and replacement of affected material if a problem occurs. |
| Dimensional Inspection |
Check how outside diameter, wall thickness, length, ovality, straightness at ends, and coil geometry are measured. |
The inspection plan should identify calibrated instruments, sampling frequency, applicable tolerances, and the recorded results for each production lot. |
Accurate dimensions reduce installation problems and ensure compatibility with connectors, heat exchangers, and forming equipment. |
| Quality Management |
Request evidence of a documented quality system and confirm whether certificates are current and relevant to the production site. |
ISO 9001 certification is a useful management-system indicator, but it should be evaluated together with product test records, process controls, calibration records, and customer-specific inspection requirements. |
A quality certificate alone does not guarantee product conformity; production evidence is also necessary. |
| Sample and Pre-Production Approval |
Obtain a representative sample or first-article coil before approving a large order. |
The sample should be checked for grade, dimensions, surface finish, coil shape, weld condition where applicable, test documentation, and fit with the intended equipment. |
Early verification reduces the risk of discovering dimensional or material problems after full-scale production. |
| Lead Time and Capacity |
Ask for production lead time, available monthly capacity, raw-material availability, inspection duration, and shipping schedule. |
The supplier should provide a written schedule with order confirmation, production completion, inspection release, packing, and dispatch milestones rather than only a general delivery estimate. |
Reliable planning helps prevent equipment downtime and project delays. |
| Packaging and Transport |
Confirm coil diameter, spool or pallet design, end protection, moisture protection, lifting points, and marking requirements. |
Packaging should prevent deformation, contamination, corrosion, and unwinding during handling. Each coil should be clearly marked with grade, size, length, heat number, and order reference. |
Proper packaging protects the tubing between final inspection and installation. |
| Total Cost of Ownership |
Compare material price together with testing, documentation, tooling, packaging, freight, duties, installation, and potential replacement costs. |
The lowest unit price is not necessarily the lowest project cost. Evaluate yield, continuous length, defect rate, delivery reliability, and documentation completeness. |
A broader cost comparison gives a more realistic view of long-term value and project risk. |
| 2026 Supplier Selection Checklist |
Score suppliers consistently before issuing a purchase order. |
Use a documented review covering material suitability, standard compliance, traceability, testing, dimensions, surface finish, capacity, delivery reliability, communication, and after-sales support. |
A structured comparison makes supplier selection more objective and reduces dependence on price alone. |